The question “Why do plastic packages need proper sealing” matters wherever product quality depends on protection. A sealed pouch can block moisture, oxygen, dust, and microorganisms. It can also prevent leakage during storage, transport, and handling. Without a reliable seal, even excellent packaging materials may fail.
In practical packaging work, small details often decide performance. Heat, pressure, and dwell time must match the plastic structure. Operators inspect seal width, wrinkles, contamination, and uneven edges. A clean seal usually looks continuous and firm. However, appearance alone cannot prove package integrity. Peel tests, burst tests, vacuum checks, and leak detection provide stronger evidence. These methods help quality teams identify weak points before products reach customers.
Consider a snack pouch exposed to humid air. Its contents may lose texture before the printed package shows damage. A liquid refill may leave only a tiny trail along a poor seal. That small leak can stain cartons and trigger customer complaints. In sensitive applications, sealing problems may also affect shelf life and safety. Packaging standards and documented procedures provide useful control, but they do not replace careful observation. Machines drift. Film varies. People occasionally miss defects.
That is the uncomfortable part. No sealing process is perfect. Reliable results require regular calibration, trained operators, suitable materials, and honest testing. Proper sealing protects more than the package itself. It preserves product value, supports traceability, and builds customer trust. Understanding the sealing process makes prevention more practical than costly correction.
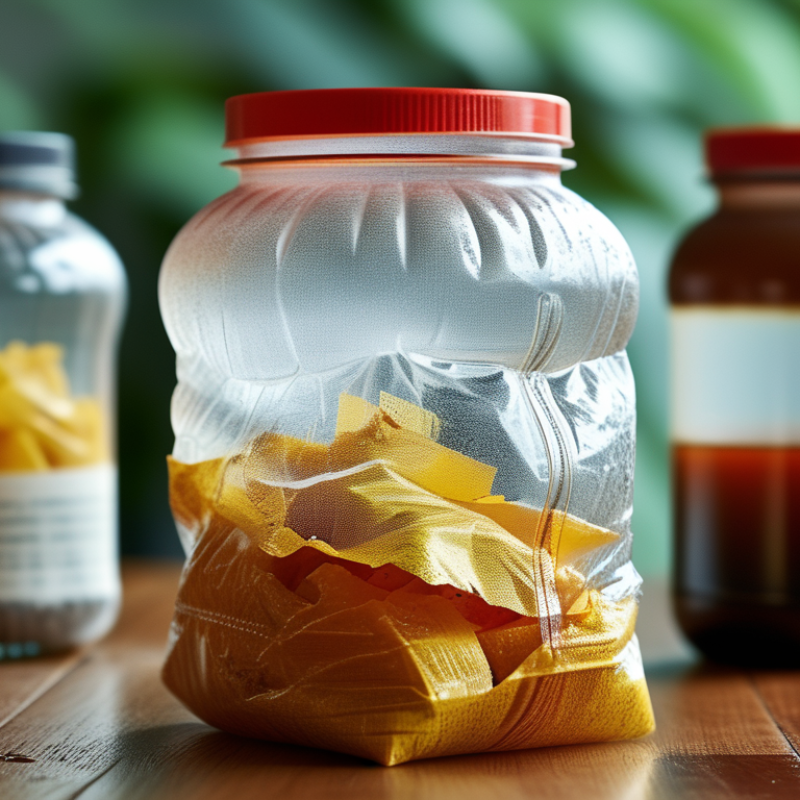
Proper sealing means creating a continuous, strong barrier between two plastic layers. It protects contents from moisture, oxygen, dust, and accidental opening. The seal must match the film structure and package design. Heat, pressure, and dwell time all affect the result. Too little heat may leave hidden channels. Too much heat can weaken or distort the film. Small changes matter.
In packaging inspections, I have seen edges that looked smooth but leaked during testing. A reliable process checks seal width, alignment, wrinkles, and contamination. Peel tests measure opening strength without hiding weak areas. Leak tests can expose tiny paths that visual checks miss. Records should include machine settings, material lots, and inspection results. Guesswork is risky.
Proper sealing also depends on the material’s condition. Clean film surfaces are essential. Dust, oil, product residue, or trapped folds can prevent full contact. Flexible packages may need different settings from rigid plastic trays. Technicians should validate each structure under expected storage and handling conditions. Relevant packaging standards can guide the test plan, but they cannot replace practical checks. No setting remains perfect forever. Equipment wears, films change, and operators make occasional mistakes. That uncertainty deserves regular review.
| Sealing Dimension | What Proper Sealing Means | Practical Data or Target | Common Verification Method | Risk When Sealing Is Inadequate |
|---|---|---|---|---|
| Seal Continuity | The seal should form one continuous, closed barrier around the package opening, with no visible gaps, wrinkles, or unbonded areas. |
100% closure required No open channels or visible interruptions across the intended seal area. |
Visual inspection, seal-profile inspection, and dye-penetration testing where applicable. | Air, moisture, microorganisms, dust, or product may enter or escape through the package. |
| Seal Width | The seal should provide enough bonded area for the package design, material combination, and expected handling load. | A seal width of approximately 3–10 mm is commonly used as a design starting range, but the final value depends on the package and application. | Dimensional measurement and seal-strength testing according to ASTM F88/F88M or an equivalent method. | A narrow or inconsistent seal can reduce strength and increase the probability of edge leaks or peel failure. |
| Seal Strength | The bonded layers should withstand opening, filling, transport, stacking, and consumer or industrial handling without unintended separation. | Strength is reported as force per unit seal width, commonly N/15 mm or N/25 mm. There is no single universal pass value for every package. | ASTM F88/F88M seal-strength test, using an application-specific acceptance limit. | Weak seals may burst during distribution; excessively strong seals may be difficult to open or may tear the package material. |
| Leak Tightness | The package should resist the movement of air, liquid, or vapor through the seal under the pressure and environmental conditions expected during use. | The acceptable leak rate is application-specific. Critical packages generally require a validated maximum leak limit rather than a visual-only inspection. | Bubble-emission testing such as ASTM F2096, vacuum decay, pressure decay, or another validated leak test. | Loss of product, contamination, oxidation, reduced shelf life, or loss of sterility may occur. |
| Clean Seal Area | The sealing surfaces should be free from product, powder, grease, liquid, fibers, and other contamination before pressure and heat are applied. | No visible contamination should cross the seal interface. The allowable contamination level should be defined during process validation. | Visual inspection, process audits, simulated-contamination studies, and leak testing. | Contamination can create microchannels that remain difficult to detect but permit leakage. |
| Temperature Control | The sealing temperature should activate the sealant layer without damaging, shrinking, burning, or distorting the package structure. | Many thermoplastic sealant systems operate within approximate ranges of 120–200°C, but the correct window must be established from the material specification and validation trials. | Calibrated temperature measurement, seal-strength testing, and inspection for scorching, distortion, or incomplete bonding. | Too little heat can cause weak bonding; too much heat can cause film distortion, brittleness, blocking, or burn-through. |
| Dwell Time | The sealing jaws or bars should remain closed long enough to transfer heat and pressure consistently across the complete seal width. | Many heat-sealing processes begin trials around 0.5–2.0 seconds, but the correct time depends on film thickness, sealant type, temperature, and equipment speed. | Machine parameter monitoring, seal-strength testing, and process-capability analysis. | Insufficient dwell time may produce incomplete bonding; excessive dwell time may slow production or damage the film. |
| Sealing Pressure | Pressure should be sufficient and evenly distributed to bring the sealant layers into intimate contact across the entire seal area. | Pressure must be validated for the specific machine, jaw design, film structure, and seal width; uniformity is more important than a nominal setting alone. | Pressure calibration, jaw-parallelism checks, pressure-sensitive film, and seal-strength mapping. | Uneven pressure can create weak spots, incomplete contact, wrinkles, and localized leak paths. |
| Seal-Surface Alignment | The intended sealant layers should overlap correctly, with the package material positioned flat and without folds or misalignment. | The actual overlap and allowable offset should be specified on the package design drawing and checked during setup and production. | Visual inspection, dimensional checks, and first-article or start-up approval. | Misalignment can reduce bonded area and produce an incomplete or irregular seal. |
| Barrier Performance | The sealed package should maintain the required resistance to oxygen, water vapor, light, aroma, or other environmental factors throughout its intended shelf life. | Oxygen transmission rate and water-vapor transmission rate are measured using standardized test conditions; target values depend on the product and shelf-life requirement. | ASTM D3985 for oxygen transmission and ASTM F1249 or ASTM E96 for water-vapor transmission, as applicable. | The product may oxidize, dry out, absorb moisture, lose aroma, or experience accelerated degradation. |
| Opening Performance | The package should open as intended: cleanly when easy opening is required, or with controlled resistance when tamper evidence and security are priorities. | Opening force and tear behavior should remain within limits established by the package design and user requirements. | Peel-force testing, tear testing, and user-handling evaluations. | An overly weak seal may open during transport; an overly strong or irregular seal may cause spillage, tearing, or user injury. |
| Process Consistency | Temperature, pressure, dwell time, jaw alignment, line speed, and material condition should remain within validated operating limits. | Critical parameters should be recorded and monitored using defined control limits. Periodic revalidation is required after significant material, machine, or process changes. | Statistical process control, equipment calibration, capability studies, and scheduled seal audits. | A process that varies over time can produce intermittent failures even when individual packages appear visually acceptable. |
| Environmental Resistance | The seal should remain functional after exposure to expected temperature, humidity, vibration, compression, chemicals, and handling conditions. | Test conditions should represent the intended distribution and storage environment, including low- and high-temperature extremes where relevant. | Aging studies, transport simulation, compression testing, temperature cycling, and post-test leak or strength testing. | A seal may weaken, embrittle, creep, or develop channels during storage or transportation. |
| Regulatory and Quality Validation | The complete package system, including materials, sealing process, and intended use, should be validated against applicable requirements. | ISO 11607-1 and ISO 11607-2 are commonly referenced for terminally sterilized medical-device packaging systems. Other sectors may require different standards. | Documented qualification, process validation, seal-strength testing, integrity testing, aging studies, and change control. | Unvalidated sealing may lead to nonconforming products, recalls, regulatory action, or loss of customer confidence. |
: A seal blocks moisture, oxygen, dust, and accidental contact. It helps preserve texture, cleanliness, odor, and product quality. Small failures can matter.
Temperature, pressure, and dwell time strongly affect the seal. Low heat may prevent proper bonding. Excessive heat can distort the film. Timing matters too.
No. Different film structures may need different settings. A suitable temperature for one material may weaken another. Testing is necessary.
Crumbs, oil, powder, wrinkles, and uneven surfaces can create leak paths. Even a tiny particle may interrupt bonding. Clean surfaces help.
Yes. A seal may appear strong while hiding a narrow channel leak. Visual inspection cannot reveal every defect. That is easy to miss.
Use leak testing and peel testing on real packages. Test samples after production begins, not only empty packages. Measured evidence is safer.
Check seal width, wrinkles, burn marks, weak corners, and material movement. Inspect the first packages from each batch. Record the results clearly.
Yes. Humidity, storage temperature, machine wear, and uneven film thickness can change results. A stable setting may fail later in the same shift. Conditions need review.
Change one setting at a time and retest real samples. Review rejected packages for movement, contamination, or pressure problems. The cause may not be heat.
Why do plastic packages need proper sealing? A reliable seal creates a secure barrier that helps protect products from moisture, oxygen, dust, microorganisms, leakage, and accidental tampering. It preserves freshness, quality, and safety throughout storage, transportation, and use. Proper sealing also supports longer shelf life and reduces the risk of contamination or product loss.
The effectiveness of a plastic package seal depends on factors such as material compatibility, sealing temperature, pressure, dwell time, package cleanliness, and the condition of the sealing equipment. Different packages may use heat sealing, ultrasonic sealing, induction sealing, adhesive sealing, or zipper-based closure systems. To check whether a package is properly sealed, manufacturers can inspect the seal visually and perform tests for leaks, seal strength, channel defects, and opening resistance. Consistent testing and suitable process control help ensure that every package performs as intended.
 Premir Plastic Package