As global commercial hubs accelerate the transition toward circular economic models, enterprise operations in Grenville require robust, economically viable, and regulatory-compliant reusable plastic packaging systems. Moving beyond single-use polymers, modern manufacturing and logistics ecosystems depend on high-tensile, thermal-resistant, and chemically inert reusable packaging to safeguard inventory, slash reorder expenditure, and meet stringent carbon mitigation mandates.
Tongcheng Packaging Materials Co., Ltd. delivers comprehensive OEM/ODM packaging engineering engineered explicitly to serve Grenville's commercial hubs, regional agricultural distribution channels, garment manufacturers, healthcare providers, and heavy industrial facilities. By integrating high-density polymers (HDPE/PP), bioplastic resins, barrier layer laminations, and advanced thermoforming processes, our factory supplies end-to-end reusable systems that guarantee structural longevity across hundreds of supply chain cycles.
Grenville’s evolving commercial sector presents complex packaging requirements spanning regional supply chain node management, localized food manufacturing, high-density warehousing, and retail fulfillment. As environmental regulations throughout the region enforce stricter limits on single-use polyolefins, enterprise procurement officers in Grenville are actively restructuring their inventory containment infrastructure.
Standardized reusable containers allow Grenville manufacturers to maximize container loading density, minimize transit damage, and streamline reverse logistics operations seamlessly.
While initial acquisition unit costs exceed single-use film bags, high-cycle durability yields up to an 82% reduction in long-term total cost of ownership (TCO) across 50+ closed-loop cycles in Grenville networks.
Designed in accordance with international ISO environmental standard frameworks, helping Grenville businesses meet ESG targets and localized zero-waste landfill protocols.
True reusable plastic packaging requires specific material science formulations to endure repeated stress-cracking forces, UV degradation, mechanical impacts, and industrial wash cycles. Our factory leverages multi-layer co-extrusion and dynamic polymer blending to maximize asset lifecycle performance.
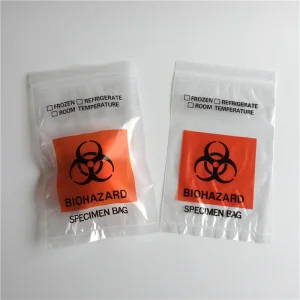
For liquid food items, sauces, biohazard clinical tubes, and chemical cleaning agents, seal integrity is non-negotiable. Our reusable packaging features custom co-extruded barrier layers (EVOH and Nylon inserts) achieving exceptional performance:
Water Vapor Transmission Rate (WVTR): < 0.5 g/m²/24h
Oxygen Transmission Rate (OTR): < 1.2 cc/m²/24h
Tensile Strength at Yield: > 32 MPa (ASTM D638 standard)
The future of reusable packaging in Grenville relies on the integration of data intelligence, material traceability, and automated reverse logistics tracking systems.
Factory-integrated RFID micro-chips and serialized QR code printing allow Grenville logisticians to track asset usage, count washing cycles, and auto-manage deposit-return schemes across distribution hubs.
Pioneering sugarcane-derived polyethylene and bio-EVA substrates that deliver 100% mechanical recyclability while reducing cradle-to-gate carbon emissions by up to 68%.
Replacing thermal adhesives with high-frequency ultrasonic weld technology, guaranteeing hermetic seals for biohazard transport containers and liquid spouted pouches.
Our engineered plastic packaging configurations are structured to resolve specific operational challenges across key commercial sectors in Grenville:
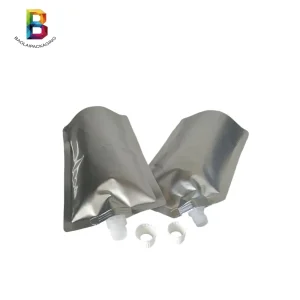
Grenville’s regional food processors require robust liquid containment and frozen food storage. Spouted stand-up pouches and heavy-duty thermoformed stone paper trays offer grease resistance, leak protection, and full washability for repeated food contact use under strict hygiene controls.
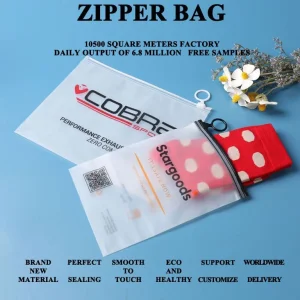
Textile operators in Grenville leverage our frosted EVA slider bags with reinforced custom zipper closures. These bags protect garments against moisture, dust, and friction damage during transit while enabling direct re-use by consumer end-users or internal inventory redistribution systems.
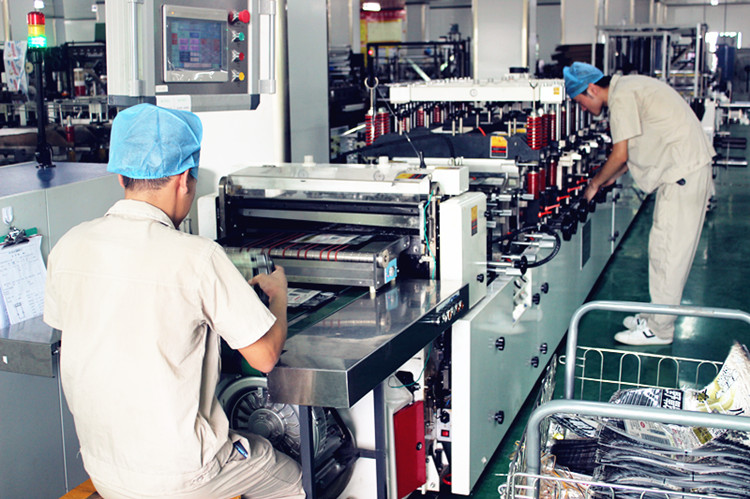
Since 1985, Tongcheng Packaging Materials Co., Ltd. is a senior professional manufacturer in supplying flexible packaging by international standards. Our products exported to countries in Europe, America and Southeast Asia. The company covers a total area of 5500 square meters and has 7700 square meters for building. The company's registered capital is RMB 11.98 million Yuan. There are totally 150 lovely employees working together. Equipped with gravure plate making, printing, lamination, slitting, bag-making and film-blowing and testing areas, our annual production capacity reached 5000 tons.
We follow quality control system of ISO22000 and GB 9683-1988 strictly to ensure quality. Based on this, our products are exported to clients all over the world. All these products are qualified after being tested by authentic system.
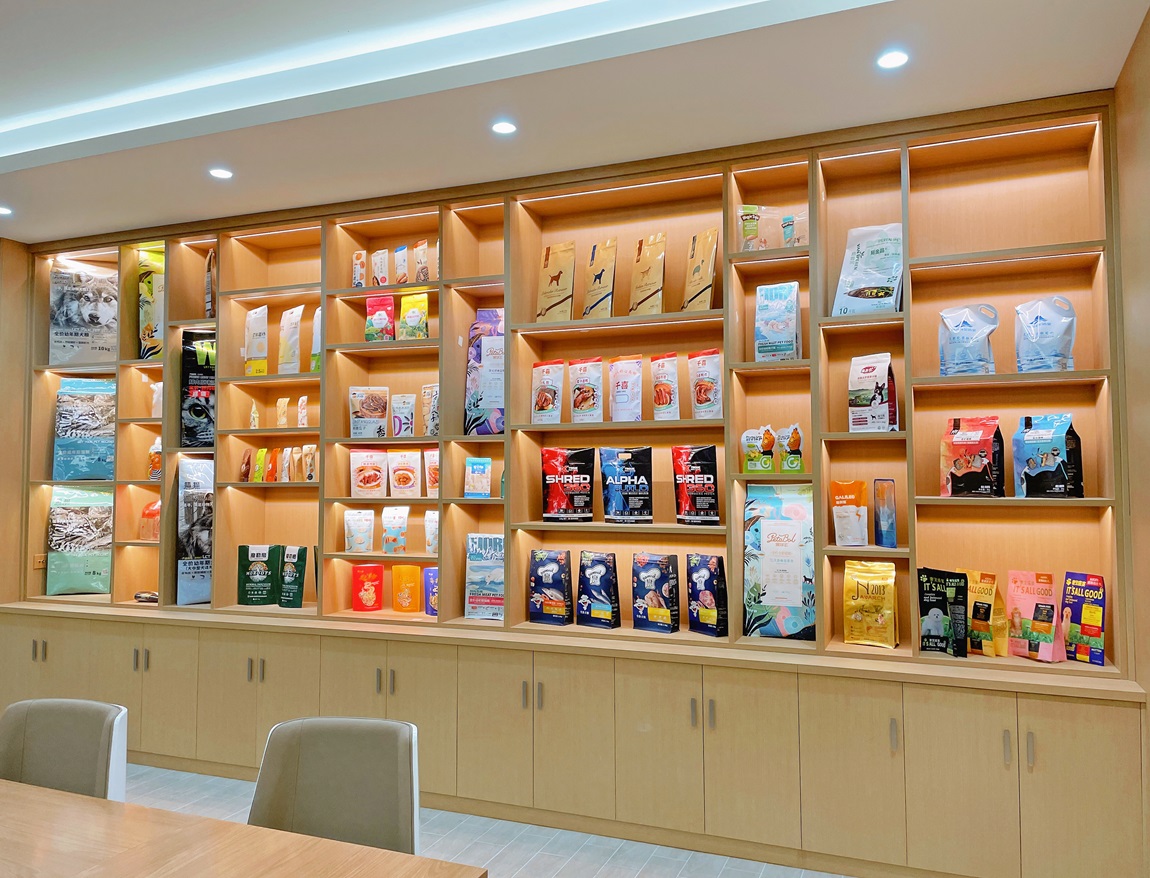
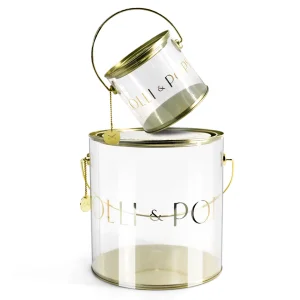
Explore our primary inventory of specialized reusable plastic packaging products, fully customizable with gravure logo printing, custom colorways, dimensional scaling, and barrier performance properties:
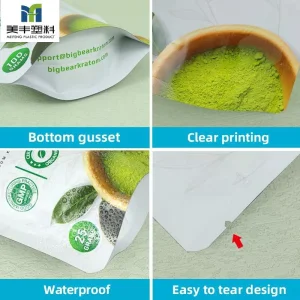
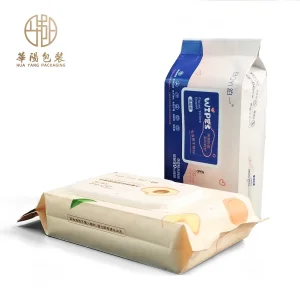
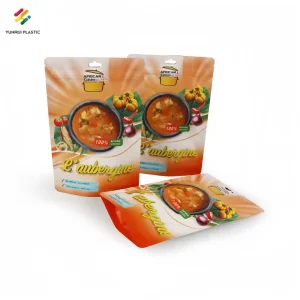
To maintain seamless compatibility with local regulatory frameworks serving Grenville and international trade corridors, our manufacturing center executes a rigorous 6-stage Quality Control Protocol from polymer resin intake to outbound container freighting.
Find authoritative engineering answers regarding custom tooling, freight arrangements to Grenville, order minimums, and sustainable material options.
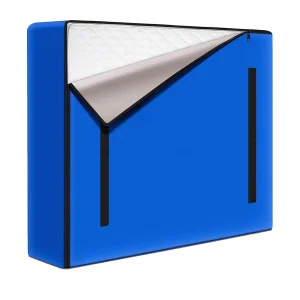
While single-use bags incur recurring per-unit procurement costs on every shipment, reusable plastic packages—such as our 180GSM heavy-duty PP mattress bags or reinforced EVA garment bags—are engineered for dozens to hundreds of reverse-logistics cycles. Over a standard 12-month operational period in Grenville distribution channels, the total cost per trip typically decreases by 60% to 80% compared to consumable corrugated or thin polyethylene wraps.
Our factory provides full OEM and ODM services. We offer custom gravure plate printing up to 8 colors, tailored dimensional sizing, specialized closure mechanisms (such as slider zippers, spout caps, or twist ties), material thickness adjustments (from 40 microns up to heavy rigid gauges), and specific resin choices including bio-degradable EVA, stone paper composites, or food-grade PET/PP.
Yes. Tongcheng Packaging operates under a strict ISO 22000 food safety management system and adheres strictly to GB 9683-1988 guidelines alongside international FDA standards. All materials used in our food-grade spout pouches, clear buckets, and thermoformed stone paper trays are 100% virgin, BPA-free, and migration-tested for safety with acidic, oily, or hot-filled food products.
Standard production lead times range from 14 to 21 business days following digital artwork approval and deposit confirmation, supported by our annual capacity of 5,000 metric tons. Freight options to Grenville include direct full-container load (FCL) sea freight, less-than-container load (LCL) consolidation, or expedited air freight for urgent commercial inventory requests.
Yes. We can integrate embedded UHF RFID labels, scannable high-density QR codes, or unique serial barcode sequences into your reusable packaging during the bag-making or laminating stage. This empowers Grenville logistics operators to automate inventory audits, track wash cycle limits, and monitor asset distribution automatically.
Connect directly with our senior packaging design engineers today. We offer structural CAD prototyping, factory-direct wholesale pricing, and full technical compliance support for your enterprise.
Send Inquiry Now Premir Plastic Package